Your single-source partner for everything valves
Vimax Technocast is a rapidly growing valve casting component manufacturer in India, with 10,000-plus successful shipments. We are PED 2014/68/EU-, AD 2000 Merkblatt W0-, and IBR-certified, and manufacture in an ISO 9001-certified facility. Our product range includes components for all leading valve types, from check and gate to butterfly and cryogenic valves. We cast in line with IS 1116:1993 and VDG P690 requirements, and meet all necessary standards, such as API 6D, ASME B16.34, EN 12266, and more.
Simplify your supply chain, compress time-to-market, and import at a port of your choosing.
Valve Components Manufacturers in India: Our Legacy
Since our inception in 2012 in Rajkot, India, we have grown from a small workshop into a leading global supplier of precision investment castings. Our mission is simple: empower your engineering success with durable valve components that excel in performance and cost efficiency.
Your challenges guide our solutions. Whether you are upgrading an aging chemical processing plant or launching a new series of subsea valves, we ensure that you cut your valve assembly costs by 18% and improve your leak-test pass rate to 100%.
View Our Valve Components Gallery


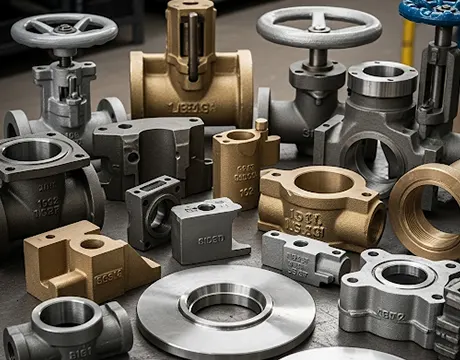
Our Range of Valve Casting Components
We produce a wide range of valve components as a premier valve castings component manufacturer in India, shipping globally.
| Valve | Valve Casting Components |
|---|---|
| Ball valve | Body, Bonnet, Ball, Actuator components, Seat retainers, End caps |
| Butterfly valve | Body, Disc, Seat retainers |
| Gate valve | Body, Bonnet, Gate/Wedge, Seat rings, Yoke |
| Globe valve | Body, Bonnet, Disc, Seat rings |
| Check valve | Body, Cover, Lift disc, Hinge arm, Disc holder, Seat ring |
| Diaphragm valve | Body, Bonnet, Compressors |
| Plug valve | Body, Bonnet, Plug, Gland components |
| Needle valve | Body, Bonnet |
| Cryogenic valve | Body, Bonnet, Flange, Closure member, Seat ring |
Valve Casting Alloys and Materials
We pour the following grades of alloys, including steel, to create valve casting components that meet and exceed performance benchmarks.
| Alloys | Grades |
|---|---|
| Carbon steel | WCB, WCC, LCC, LCB |
| Low-alloy steel | WC1, WC4, WC5, WC6, WC9, WC11, C5, C12, C12A |
| Martensitic steel | CA15, CA40, CA-6NM |
| Austenitic stainless steel | CF8, CF8M, CF3, CF3M, CF8C, CF10, CK20, CH20, CN7M |
| Heat-resisting steel | HF, HH, HI, HK, HD |
| Austenitic ferritic duplex steel | CF3MN, CD4MCu, GC6MMN, CK3MCuN |
| Duplex & Super duplex stainless steel | A890 (1A, 2A, 3A, 4A, 5A, 6A) |
| Nickel-based superalloys | M-35-1, M-30-C, N-12-MV, CY40, CW12MW, CW6M |
| Cobalt-based alloys | Stellite 6, Stellite 21, Haynes 25, Haynes 188, MP35N |
For a complete list of all the materials and grades we pour with, please visit our materials details page.
Technical Details
As valve castings component manufacturers, we produce a range of components with varied thickness, weight, and tolerance.
| Particulars | Details |
|---|---|
| Process | Investment casting, Lost-wax casting |
| Shell building media | Ceramic, Stucco |
| Induction furnace | 250 kWh |
| Crucible capacity | 100 kg, 300 kg |
| T-spout ladle capacity | 35 kg, 50 kg, 80 kg |
| Casting weight range | 0.04 – 150 kg |
| Max dimension | 900 x 900 x 450 mm |
| Wall thickness | 1.5 – 5 mm |
| Surface roughness | N9–N7 (Ra 6.3–1.6 μm) |
| Machining allowance | 0.3 – 1 mm |
| Tolerance | DCTG 4–7, GCTG 3–6 |
| Surface treatment | Electropolishing, Passivation, Powder Coating, Shot blasting |
| Heat treatment | Solution annealing, Quenching, Normalizing, Tempering |
| Compliance & standards | ASME B16.34, ASME B16.10, ASME B16.47, EN 12516, MSS SP-25, API 598, ISO 5208, EN 12266, MSS SP-61, API 6D, ASTM, NACE |
Our Valve Castings Component Manufacturing Process
At Vimax, our valve castings are produced in a state-of-the-art facility, where precision and quality control are integrated throughout the manufacturing process.
Wax design
Injecting wax into engineered moulds to form the wax patterns. Each component is aligned carefully and attached to a sprue to form the wax pattern tree.
Shell formation
Dipping the wax pattern tree into the hot pot, followed by a stucco coating in the rainfall sanders. This coating-drying-coating-drying process is repeated up to eight times to create a strong ceramic shell.
Shell heating
Placing the ceramic shells in an autoclave, where hot steam quickly liquefies the wax, leaving behind a perfect negative impression. The shell is then placed in a pre-heated furnace to remove residual moisture and leftover wax.
Pouring
Introducing the molten alloy into the ceramic shell. The molten metal occupies the negative space and gradually cools down to form valve components. Our gate design and pouring mechanism ensure minimal hot corners.
Knocking & Fettling
Breaking the shells to extract the cooled components. Sawing off the parts from the sprue, grinding down the gate stubs, and sandblasting or solution treating any residual ceramic.
Heat treatment
Putting the components in induction furnaces to heat them, followed by air cooling. This redistributes grains and improves physical properties.
Machining
Improving tolerances using HMCs and VMCs. Milling, reaming, and drilling all mating surfaces and critical surfaces to ensure excellent performance.
Final Inspection
X-ray, Spectrometric analysis, Dye-penetrant testing; impact, hardness, toughness, and other metallurgical and dimensional checks to ensure product integrity and quality assurance.
Why Choose Vimax for Valve Casting Components
Vimax Technocast brings more than 12 years of experience supplying valve casting components to valve OEMs and tier-1 suppliers worldwide. Here’s why customers across global markets trust us.
DFM
Manufacturing is faster because our in-house team iterates on your drawings to reduce weight and simplify design.
Quality materials
Pre-approved raw materials supplier list, with a strict focus on mill test certificates to ensure quality control at source.
Certification
We are PED 2014/68/EU, AD 2000 Merkblatt W0, and IBR-certified.
Modern foundry
State-of-the-art ISO 9001:2015-certified foundry with modern equipment, trained personnel, and a well-equipped testing laboratory for on-time and quality-controlled output.
Scalable infrastructure
Multiple furnaces, pouring junctions, hot pots, and a large workforce to deliver additional output during peak demand, on short notice.
Turnkey solution
From designing and prototyping to volume production, inspection, and delivery—we provide all of it to ensure supply chain simplicity and lower total cost of ownership.
Export
As valve castings component exporters in India, we ship to leading countries, including the U.S.A., Canada, the U.K., France, Germany, Poland, Italy, Spain, Saudi Arabia, the U.A.E., Japan, Australia, and New Zealand, with compliance requirements considered for each market.
Sustainability
Solar power plant to meet up to 60% of energy requirements, best manufacturing practices to reduce wastage, and other production procedures that help reduce carbon emissions.
“Vimax Technocast has consistently delivered on our requirements for valve components. We are quite pleased with the quality of their product, since they lower our machining costs. But what’s best is their ability to meet our ad hoc requirements at lower turnaround times. We greatly appreciate that.”
Procurement Manager
Tier-1 Supplier, Saudi Arabia
Looking for Valve Castings Component Exporters India?
Whether you are sourcing a new valve component or evaluating an existing design, our technical team can help you assess your requirements and discuss the right casting solution.
Applications of Our Valve Casting Components
Our valve castings are routinely used as end-products in the following industries:
- Oil & Gas: Ball, gate, and globe valve components, including valve bodies, are used to handle crude, natural gas, and refined products in upstream wellheads, pipelines, and refinery processes under high pressure.
- Chemicals & Petroleum: Corrosion-resistant valve bodies are instrumental in handling acids, solvents, and hydrocarbons across reactors and storage systems.
- Paper & Pulp: Knife gate valve components help handle demanding pulp slurry, black liquor, and other liquid process discharges.
- Wastewater: Gate and knife gate valve components help control the flow of viscous sludge and dissolved media, enabling localized wastewater treatment.
- Energy: Routinely used to control the flow of water, steam, and coolants in thermal, solar, and hydroelectric plants.
- Railways: Valves are used in loco sheds, along maintenance lines, and in locomotives for cleaning and coolant circulation.
FAQs
Do you manufacture all types of valve casting components?
We only produce castings that can be manufactured via investment casting. These are usually complex parts or seamless components, for which billet machining is not economically feasible.
Do you cast all types of alloys and materials?
We pour all major alloys and materials that are conducive to investment casting. This includes staples such as stainless steel and uncommon superalloys.
Can you pour with custom alloys?
As experienced investment casting manufacturers, we can pour your proprietary alloy. We have IP protection mechanisms in place to ensure your composition remains yours, well after the project finishes.
What lead times do you offer?
The standard lead time for a casting project is between 25 and 40 days for the first dispatch. Subsequent dispatches take less time, subject to conditions.
Do you export valve casting components to other countries?
We export worldwide. To learn whether we ship to a port of your choosing, please get in touch with us.